A blank operator panel during a production run does not always mean the HMI itself has failed. When engineers ask what causes HMI screen failure, the answer can range from a failed 24 VDC supply to a damaged touch overlay, a loose communication lead, corrupted project data or a fault elsewhere in the control cabinet. Identifying which layer has failed matters before a replacement part is ordered.
An HMI is the operator's view of the machine, but it is also an electronic device operating in heat, vibration, electrical noise and often demanding shift patterns. Treat the symptoms as evidence. Is the display dark? Is it lit but frozen? Does the touchscreen not respond? Does the panel start normally but show communication alarms? Each outcome points to a different fault path.
What causes HMI screen failure in industrial equipment?
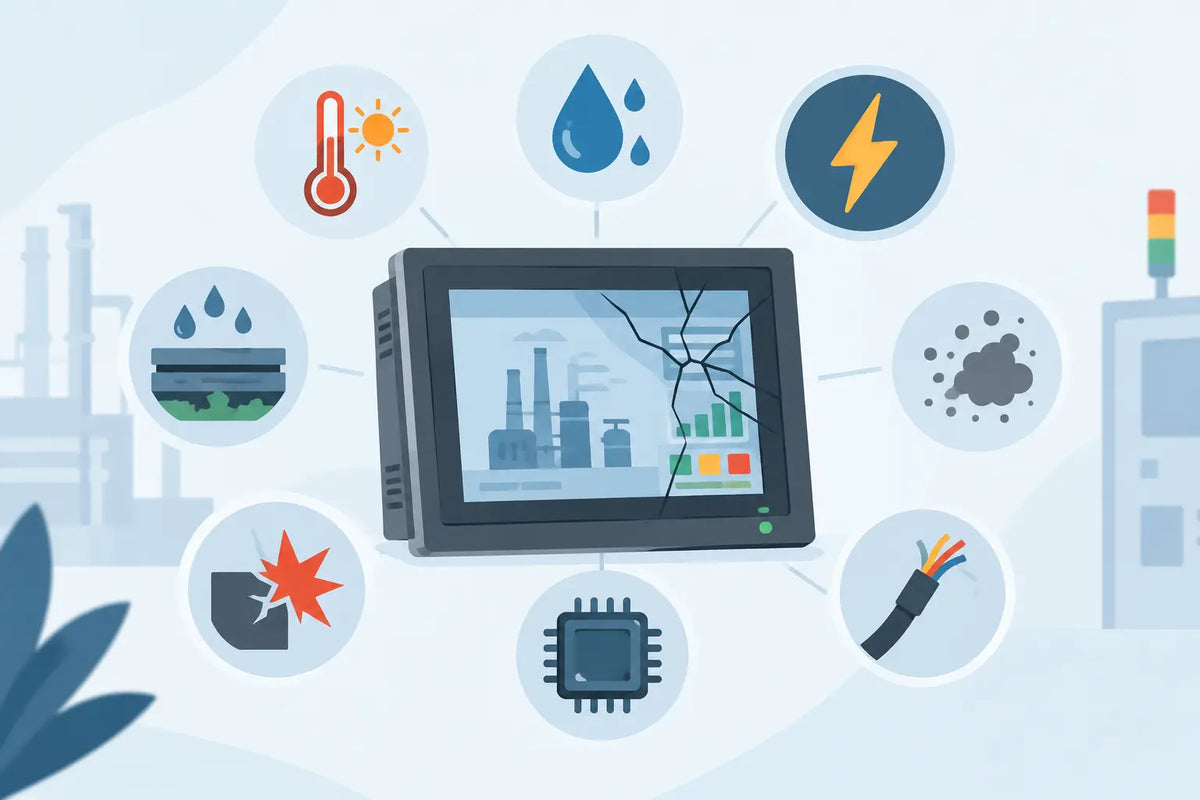
Most HMI faults fall into one of eight practical categories. Some can be corrected at the machine; others require repair or replacement. The key is to avoid treating every unresponsive panel as a display fault.
1. Loss of power or unstable DC supply
A completely black screen is often a power issue first. Check the supply voltage at the HMI terminals under load, not only at the power supply. A weak 24 VDC supply, high-resistance terminal, blown fuse, loose conductor or failing DC-DC converter can prevent normal boot-up.
Voltage dips are particularly easy to miss. The HMI may start when the cabinet is quiet, then restart or go blank when contactors, solenoids or drives energise. Review the supply capacity, earthing arrangement and any signs of heat at terminals. If several 24 VDC devices are affected together, the HMI is unlikely to be the root cause.
2. Failed backlight or display assembly
If status LEDs are active and the HMI appears to boot but the screen is very dim or black, the backlight or display circuitry may have failed. On older panels with CCFL backlights, lamp and inverter wear is a common end-of-life issue. Newer LED-backlit units can still develop driver or LCD failures.
A faint image visible under a torch is a useful clue that the processor is running and the backlight is not. That does not make field repair the right option. For a critical machine, the usual decision is between a specialist repair and a like-for-like replacement, based on lead time, cost, remaining panel condition and availability of the application backup.
3. Touchscreen or membrane damage
A screen can look normal yet be unusable because the touch layer has failed. Dead zones, false presses, drifting touch points and a panel that only responds after repeated presses usually indicate a touchscreen, overlay or calibration problem.
Oil, cleaning chemicals, moisture and physical impact all shorten the life of the front interface. So does constant use of one area of the screen, such as an acknowledgement button. Cracked overlays also compromise the enclosure rating, allowing contaminants to reach internal electronics. If the HMI is mounted where washdown, dust or coolant exposure is routine, examine the bezel gasket and enclosure integrity as well as the panel face.
4. Heat, ventilation and component ageing
HMI electronics generate heat, and cabinet temperature has a direct effect on their service life. Blocked filters, failed enclosure fans, direct sunlight and proximity to drives or transformers can push a panel beyond its rated operating temperature. Common symptoms include intermittent blanking, random resets, fading display brightness and failure after a warm-up period.
Electrolytic capacitors and power-board components age faster in hot cabinets. A panel may run reliably for years, then become unstable during summer temperatures or after changes to the cabinet layout. Record ambient temperature and compare it with the HMI manufacturer's rating before condemning the unit.
5. Vibration, loose connections and physical shock
Repeated machine vibration can loosen plug-in connectors, damage solder joints and fatigue cable conductors. This is especially relevant on presses, conveyors, packaging lines and mobile equipment. A panel that cuts out when the cabinet door moves, or changes behaviour when a cable is touched, needs a careful connection check.
Inspect the power plug, Ethernet or serial connector, earth bond and panel mounting hardware with power isolated. Do not repeatedly reseat live connectors in an attempt to recreate the fault. That can introduce communication errors or damage ports, particularly where static discharge or poor earthing is present.
6. Electrical noise, earthing and surge damage
Variable speed drives, switched inductive loads and poor cable segregation can cause electrical interference that looks like an HMI failure. The display may freeze, the touch input may act unpredictably, or communications may drop out during motor starts. A surge following a power event can also damage communication ports or the HMI power section.
Check whether the fault began after electrical work, a lightning event, a drive replacement or a change in switching loads. Verify that screen and communication cables are routed correctly, the panel is properly earthed and suppression is fitted where required. It depends on the installation, but replacing the HMI without correcting the source of interference can result in the same failure returning.
7. Corrupt application files or firmware problems
An HMI with a working screen may fail at the software layer. It might remain on a boot logo, show a runtime error, load an old project or repeatedly reboot. Corrupt memory, interrupted firmware updates, incorrect project transfers and incompatible firmware revisions are typical causes.
Before loading software, identify the full catalogue number, hardware revision, firmware version and communication configuration. Keep a verified copy of the machine application and document any IP addresses, node settings, recipes and user accounts. Loading the wrong project can stop the operator terminal communicating with the PLC even though the replacement hardware is healthy.
8. PLC or network communication faults
A message such as “PLC not responding” does not necessarily mean the HMI has failed. In this situation, the display and touch interface may be fully operational. The problem could be a PLC power loss, processor fault, network switch issue, broken Ethernet lead, duplicate IP address, serial setting mismatch or changed controller configuration.
Start by confirming the HMI is running its application. Then check the controller status, network link LEDs, cable condition and port configuration. If another device on the same network is communicating normally, that narrows the investigation. For serial systems, verify baud rate, parity, station address and correct cable pinout rather than assuming a standard lead will work.
A practical fault-isolation sequence
Before removing an HMI, establish whether the fault is power, display, touch, application or communication related. Check incoming voltage at the panel, inspect connectors and enclosure conditions, and note all LEDs, error messages and boot behaviour. Photographs of the screen and wiring before removal can save time later.
If the unit powers but does not communicate, test the controller and network separately. If the touchscreen alone is faulty, decide whether the machine can be operated safely through another approved method while parts are sourced. Never bypass interlocks or use an improvised operator control method simply to keep production moving.
For intermittent faults, record the conditions when they occur: time after start-up, cabinet temperature, motor operation, washdown, door movement or a particular production recipe. This evidence is more useful than a general report that the screen “sometimes goes off”.
Ordering the right replacement HMI
Part-number accuracy is central to a fast replacement. Record the complete model number from the unit label, including suffixes, series or generation, display size, supply voltage and communication ports. A visually similar Siemens, Allen-Bradley, Mitsubishi, Schneider or Omron panel may not accept the same project or fit the same cut-out.
Confirm whether the existing application can be transferred and whether a replacement needs matching firmware. Legacy systems may require an exact unit because a newer generation changes engineering software, memory format or interfaces. In other cases, a current model can be a sensible upgrade, but it should be planned rather than selected during an unverified breakdown.
New and sealed stock may suit sites that require a particular condition or traceable internal procurement route. Refurbished stock can be a practical option for discontinued panels or urgent legacy repairs, provided the part number, condition and compatibility are clearly confirmed. Automation Planet UK can assist with part-number-specific sourcing across major automation brands when an exact replacement is difficult to locate.
The best spare is not simply the cheapest available panel. It is the unit that matches the machine, arrives in time, can run the correct application and returns the line to a controlled operating state. Keep the HMI project, settings and full part number with the machine documentation, and the next screen failure becomes a purchasing task rather than a prolonged investigation.