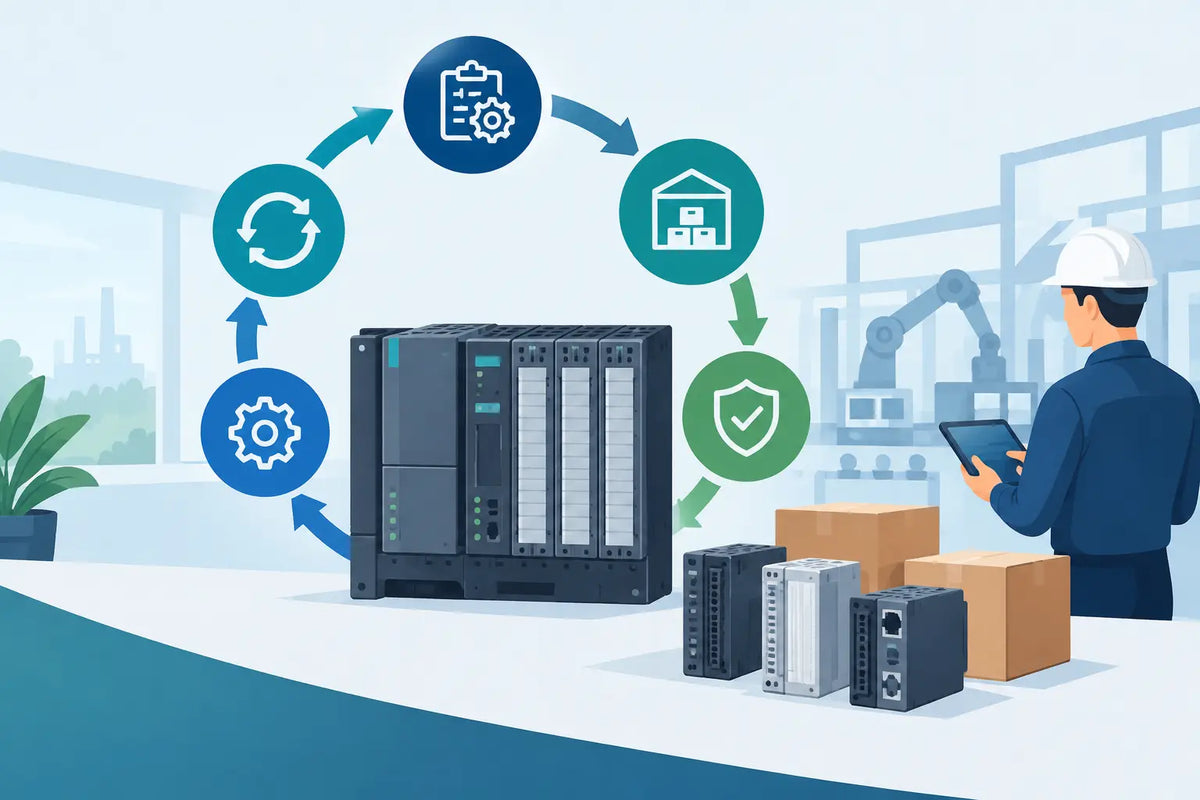
A failed CPU is rarely just a failed CPU. If the exact replacement is obsolete, the programme is unavailable, the I/O rack has changed revision, or the power supply is also near end of life, a routine repair can stop a production line for days. Managing the PLC lifecycle turns that risk into a planned purchasing and maintenance task rather than an urgent search for unavailable stock.
For maintenance teams, controls engineers and MRO buyers, the objective is straightforward: keep the installed control system supportable for as long as it remains commercially sensible, then migrate it on a timetable that protects production. That requires more than knowing which PLC brand is installed. It requires accurate part numbers, condition records, tested spares and a clear view of what will become difficult to source.
What the PLC lifecycle means in practice
The PLC lifecycle covers the period from system selection and commissioning through routine maintenance, product discontinuation, migration and eventual removal. Manufacturers may describe stages differently, but procurement decisions usually become more urgent at the same points: when a product is current, when it is mature but still supported, when it is discontinued, and when it is no longer repairable or available through normal channels.
A current platform is normally the easiest stage to support. Parts are still in production, firmware information is available and lead times are generally predictable. That does not mean there is no exposure. A plant with one critical processor and no spare can still lose output after a single electrical fault.
At the mature stage, availability may remain good while the manufacturer encourages customers towards a newer family. This is often the best time to decide whether to buy strategic spares, standardise a replacement arrangement or budget for an upgrade. Waiting until formal end of life can turn a controlled purchase into a premium-priced emergency requirement.
Once a controller or module is discontinued, the system may continue operating reliably for years. The issue is not that it must be replaced immediately. The issue is that compatible replacements, memory cards, communication modules and specialist programming equipment can become harder to obtain. A discontinued PLC can be viable when it is well documented and supported by stock. It becomes a serious risk when no one can confirm the installed part number or recover the programme.
Start with the installed base, not a generic product family
“Allen-Bradley PLC”, “Siemens PLC” or “Mitsubishi module” is not enough information to buy a safe replacement. A procurement record should capture the full manufacturer part number, hardware revision where relevant, firmware version, installed location, function and any associated accessories. For a critical rack, record the CPU, power supply, I/O modules, communications cards, rack or base, memory device and cables that could prevent a fast return to service.
This level of detail matters because near-identical modules can have different voltage ratings, terminal styles, network support or firmware requirements. A module from the same family may physically fit but fail to communicate correctly or may require programme changes. Part-number control protects against wasted purchasing and delayed repairs.
It is also worth identifying which components are genuinely production-critical. A spare analogue input card may be useful, but it does not deserve the same attention as the only processor controlling a bottling line, furnace, packaging cell or safety-related sequence. Rank assets by the operational consequence of failure, the time needed to replace them, and the likelihood that a substitute can be sourced quickly.
Keep the programme with the hardware record
A replacement PLC is only useful if the programme can be loaded and verified. Store the latest validated copy of the application, relevant software version, communications settings, passwords, drawings and backup procedure in a controlled location. Confirm that the backup is readable rather than assuming it is.
For older systems, the programming software may be as important as the spare hardware. A laptop update, expired licence, missing serial adaptor or unavailable cable can slow recovery even when the correct CPU is on site. Test the restoration process during planned downtime where possible. A recovery procedure that has never been tried is an assumption, not a plan.
Build a spares strategy around recovery time
The right spare holding depends on downtime cost, installed quantity, component availability and technical complexity. There is no universal rule that every part needs a shelf spare. Holding ten low-risk modules that can be purchased next day may tie up budget better used on one obsolete processor that has a twelve-week or uncertain replacement lead time.
For critical equipment, a practical starting point is to hold a compatible CPU, power supply and the highest-risk communications or specialist I/O module. Where several identical machines use the same rack architecture, a shared spare can be sensible. Where a line uses a unique legacy controller, a dedicated spare is usually easier to justify.
New and sealed stock offers clear condition assurance where it is available. Refurbished stock can be a cost-effective option for legacy systems, particularly when a platform has been out of production for years. The decision should reflect the asset’s role. For a non-critical replacement, refurbished hardware may be the right commercial choice. For a high-consequence application, buyers may prefer new and sealed stock, a tested spare held on site, or both.
Whatever condition is selected, receive and inspect the item before an emergency occurs. Check the label, revision, physical condition and compatibility against the installed unit. If site procedures permit, carry out a controlled bench or planned-change test. A boxed part number is not the same thing as a proven recovery spare.
Treat discontinuation as a sourcing issue and a migration trigger
End-of-life notices should start a review, not automatically force an immediate migration. An older PLC may remain suitable where the process is stable, the programme is documented and enough spare coverage exists. Replacing a functioning system can introduce commissioning risk, operator retraining and production disruption.
The balance changes when multiple parts are obsolete, programme knowledge has left the business, failures are becoming more frequent, or a required upgrade affects network security and supportability. At that point, continuing to buy one-off legacy parts may cost more than a planned modernisation.
A sensible approach is to separate short-term continuity from long-term replacement. Secure the parts needed to protect uptime over the next 12 to 24 months, while engineering defines the target platform, conversion scope, testing requirements and shutdown window. This avoids the false choice between replacing everything immediately and doing nothing until a failure forces the decision.
For multi-brand sites, avoid assuming that one supplier or one manufacturer route will cover every requirement. Plants often contain Siemens, Allen-Bradley, Omron, Schneider and Mitsubishi equipment across different lines and expansion phases. Independent sourcing can help locate exact legacy part numbers, compare new and refurbished condition options, and consolidate urgent requirements where authorised routes have long lead times or no remaining supply.
Control changes that shorten service life
Many PLC lifecycle problems are created after commissioning. An undocumented firmware update, a substitute I/O module, a revised network setting or an edited programme can leave the plant with a system that no longer matches its drawings or spare inventory. The hardware may still run, but recovery becomes slower because the recorded configuration is no longer accurate.
Use change control proportionate to the risk. After any control-system change, update the as-built documentation, programme backup, revision record and approved-spares list. If a replacement part is introduced because the original is unavailable, record what was fitted, why it was accepted and whether further changes are required. This is particularly valuable when shifts, contractors and maintenance teams share responsibility for the equipment.
Environmental conditions should also be part of the review. Heat, cabinet contamination, poor earthing, unstable power and battery neglect can reduce the useful life of otherwise reliable hardware. Addressing those faults may deliver more uptime than replacing a controller simply because it is old.
Use surplus stock as part of the plan
Surplus automation stock often sits in stores after line changes, site closures or standardisation projects. Some of it may be obsolete to one plant but exactly what another operation needs. Maintaining a clear surplus list helps prevent useful stock from being scrapped, misplaced or written off without review.
Before disposing of surplus, verify the part number, condition, quantity and any test history. Stock that is no longer relevant to your installed base can be sold and redirected into the secondary market, helping recover value while supporting other sites with legacy equipment. Automation Planet UK LTD buys surplus automation inventory as well as supplying multi-brand components, which can make this a practical route when stores need clearing without treating every old module as waste.
The best time to manage a PLC is when it is working normally and the plant has options. Keep exact records, test recovery assumptions, buy critical spares before availability tightens, and schedule migration before urgency writes the specification for you.